Project Gallery
Ambaflex Spiralveyor SV Vertical Spiral Conveyor
Description
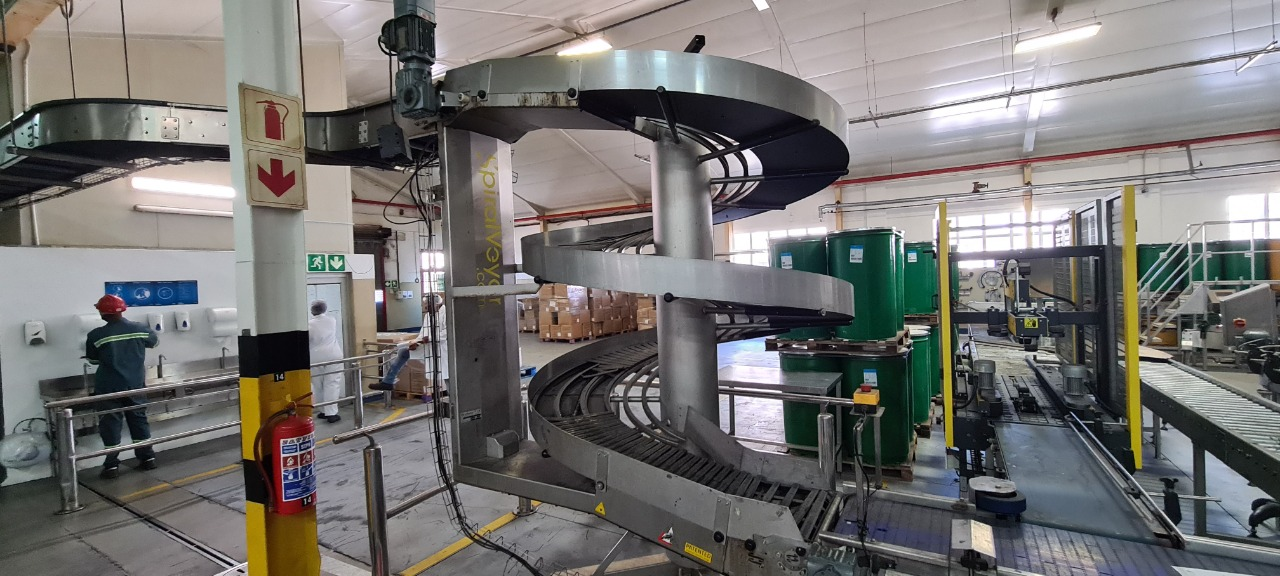
This Ambaflex Spiralveyor SV is a vertical spiral conveyor system designed for the continuous transportation of products between different levels within an industrial production, packaging, processing, or material-handling line. Manufactured by Ambaflex in 2013, the machine is identified on its nameplate as Type: SPIRALVEYOR SV with Machine No. 15080-01. The equipment is designed around a compact vertical conveying principle that allows products to be elevated or lowered while making efficient use of available factory floor space. The Ambaflex Spiralveyor SV uses a continuous spiral conveyor arrangement wrapped around a central vertical support column. Instead of transporting products horizontally over a long distance and then using separate lifting equipment, the spiral configuration allows products to travel vertically through multiple levels while maintaining a continuous conveying path. This makes the system particularly useful where production lines operate at different elevations or where available floor space needs to be used efficiently. The main conveyor structure consists of a vertical central column surrounded by a multi-level spiral conveyor track. The conveyor follows a controlled helical path around the column, creating a compact vertical transportation system. Products can enter the spiral conveyor at one level and travel continuously around the spiral until reaching the required discharge level. Depending on the line configuration, the system can be used for either upward or downward product transportation. The spiral conveyor incorporates a continuous conveying surface designed to support products as they move around the vertical path. Its construction allows products to remain within a controlled conveying route while changing elevation. The design is especially valuable in automated production facilities because it can connect equipment positioned on different floors, platforms, or line elevations without requiring a large conventional inclined conveyor. The Spiralveyor SV is particularly suited to applications where continuous product flow is required. It can be integrated into production lines between processing equipment, packaging machinery, inspection stations, storage areas, palletizing systems, and other conveyor systems. By providing vertical product transfer, the machine can act as an important connecting element within a larger automated material-handling system. The compact spiral arrangement is one of the primary advantages of this type of conveyor. A conventional inclined conveyor may require a long horizontal footprint to achieve the necessary elevation change, whereas a spiral conveyor achieves the same vertical movement within a comparatively compact area. This allows manufacturers to make better use of factory floor space while maintaining continuous product movement. The conveyor is constructed around a substantial vertical support arrangement that provides stability to the spiral track. The central structure supports the various sections of the conveyor and maintains the geometry of the conveying path. The spiral design is engineered to provide a consistent product route throughout the elevation change. An integrated drive system powers the conveyor movement. The drive assembly controls the continuous movement of the conveying surface and enables products to travel through the spiral at a controlled speed. Proper speed control is important when integrating the Spiralveyor with upstream and downstream production equipment because the conveyor must maintain a suitable product flow rate throughout the production process. The system also incorporates electrical cabling and control components associated with the conveyor drive and safety systems. Electrical connections are routed around the machine and its supporting structure to provide power and control to the conveyor drive and associated components. These systems allow the conveyor to operate as part of an automated production line rather than requiring manual product movement. Safety is an important part of the conveyor installation. The spiral conveyor is surrounded by suitable access barriers, handrails, protective structures, and controlled working areas. These features help separate the moving conveyor mechanism from personnel and provide safer access around the equipment during operation, inspection, and maintenance. The machine's 2013 manufacturing year and machine number 15080-01 are clearly identified on the manufacturer plate. The same plate identifies the manufacturer as Ambaflex and specifies the equipment type as Spiralveyor SV. The machine carries a CE marking, indicating that the equipment was manufactured and supplied with conformity marking applicable to the relevant European regulatory framework at the time of manufacture. The Ambaflex Spiralveyor SV can be used for transporting a wide variety of manufactured products, packaged goods, containers, cartons, trays, and other suitable items. The exact product range depends on the conveyor configuration, belt or conveying surface, product dimensions, product weight, line speed, and the requirements of the connected production equipment. In industrial production environments, spiral conveyors are commonly used to connect different stages of a manufacturing or packaging process. For example, products can arrive from a horizontal conveyor, enter the spiral at a lower level, travel continuously upward through the spiral, and exit onto another horizontal conveyor positioned at a higher level. The same principle can be applied in reverse for controlled downward product movement. The system is also suitable for applications where production equipment is arranged around a multi-level manufacturing layout. Instead of requiring separate lifting equipment, the spiral conveyor can provide a continuous connection between production stages. This can simplify material flow and help maintain an uninterrupted production process. The vertical conveying principle also reduces the need for manual handling between different elevations. Products can remain within the automated conveyor system while changing levels, reducing unnecessary movement and helping maintain a consistent production flow. This is particularly valuable in high-throughput manufacturing and packaging environments where products need to move continuously between multiple processing stages. The surrounding installation is configured as a professional industrial production and material-handling environment, with multiple conveyor lines and processing equipment connected around the Spiralveyor. This type of integration demonstrates how a vertical spiral conveyor can function as part of a larger automated production system, transferring products between separate sections of a production line. The conveyor's stainless-steel and industrial-grade structural elements make the system suitable for demanding production environments where cleanliness, durability, accessibility, and continuous operation are important considerations. The equipment can be incorporated into production environments with appropriate cleaning, inspection, maintenance, and operational procedures according to the specific application. Maintenance of a Spiralveyor system generally involves inspection of the conveyor surface, drive components, bearings, guide systems, structural connections, electrical wiring, safety devices, and other moving components. Regular inspection helps maintain smooth product movement and reduces the risk of unexpected interruptions in an automated production line. The machine can also be integrated with sensors and production-line controls to coordinate product entry and discharge. Such integration allows upstream and downstream machinery to communicate with the conveyor system and maintain an organized flow of products. Depending on the complete installation, sensors can be used for product detection, accumulation control, line synchronization, and operational safety. The spiral configuration provides a practical solution when a production facility requires vertical product transportation without occupying a large amount of floor space. This makes the equipment useful in facilities where production lines are densely arranged or where horizontal conveyor runs would require excessive floor area. The Ambaflex Spiralveyor SV therefore serves as an important material-handling component rather than a standalone processing machine. Its primary purpose is to move products efficiently and continuously between different elevations while maintaining connection with automated production and packaging equipment.